 Digestate Dewatering Systems
Solid Liquid Separator System
Advanced digestate dewatering and sludge separation technology. Designed with high-torque screw presses to recover dry solids and nutrient-rich liquid.
Advanced Digestate Treatment & Slurry Separation Technology
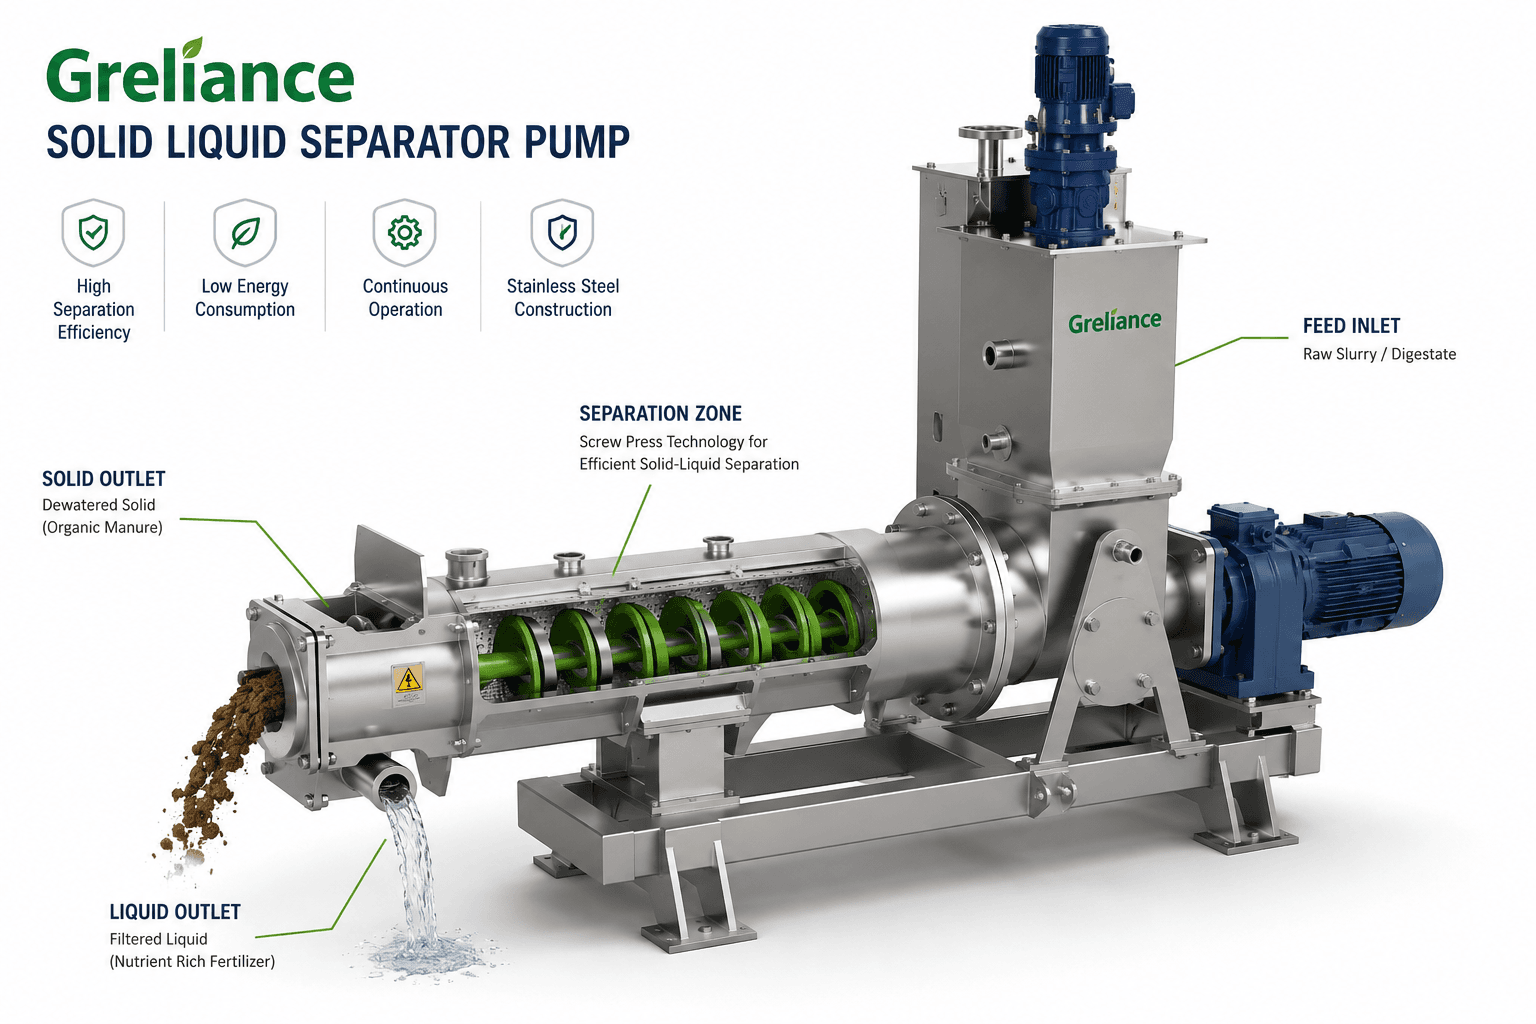
The Solid Liquid Separator System is a high-performance industrial solution designed for efficient separation of solid and liquid phases from digestate, slurry, manure, sludge, and organic waste materials. Engineered for continuous operation, the system helps BIO-CBG plants, biogas facilities, wastewater treatment units, and dairy farms improve digestate management and fertilizer recovery.
Designed with robust stainless steel construction and advanced screw press technology, the Greliance separator system delivers reliable dewatering performance with low operating cost and minimal maintenance.
Digestate Phase Transformation
The Greliance Separation System transforms raw digestate into two valuable output phases:
Solid Phase
Perfect organic soil conditioner that is easy to store and transport. Features a highly reduced odor profile and is suitable for commercial compost and organic fertilizer applications.
Liquid Phase
Nutrient-rich liquid fertilizer suitable for direct crop fertigation systems. Reduced solid contents make pumping, recirculation, and storage lagoon management extremely smooth.
Key Features
Greliance Solid-Liquid Separation systems are constructed using premium industrial specs to ensure 24/7 durability.
High Separation Efficiency
Efficiently separates digestate slurry, cow dung, poultry waste, organic sludge, fibrous biomass, and industrial slurry.
Heavy-Duty SS Construction
Manufactured using corrosion-resistant stainless steel materials (SS304/SS316) for long service life and reliable industrial performance.
Advanced Screw Press
Special wear-resistant screw systems ensure smooth material flow, stable pressure, reduced clogging, and better dewatering.
Continuous Automatic
Designed for 24x7 industrial operation with low manpower requirements and integrated safety parameters.
Self-Adjusting Pressure
Maintains stable back-pressure during separation for consistent, moisture-controlled dry output quality.
Low Power & Space
Energy-efficient drive system reduces operating expenses. Space-saving footprint fits easily into existing setups.
Working Principle
The raw slurry or digestate enters the separator unit through the inlet chamber. Inside the machine, a rotating screw conveyor compresses the material against a filtration screen.
Applications
Digestate dewatering, slurry separation, fertilizer recovery.
Cow dung separation, manure handling, organic composting.
Digestate treatment, solid-liquid separation, nutrient recovery.
Sludge dewatering, industrial treatment, effluent management.
Greliance Separation Range
We offer multiple machine setups customized for varying substrate flow structures.
Greliance Vertical Separator
Specially designed for low-fibre digestates and irregular slurry materials. Features a stable feeding system and compact footprint.
Greliance Horizontal Separator
Suitable for fibrous digestate, corn silage slurry, and cow manure applications. Equipped with a wear-resistant screw system.
Greliance Compact Separator
Ideal for small biogas plants, compact installations, and limited-space farm applications. Highly energy-efficient and low maintenance.
Submersible Chopper Pump
Designed for handling slurry containing fibers, lumpy solids, and organic wastes. Pumping and shredding are combined in one system to prevent clogging.
Micro-Filtration System
Provides fine filtration of liquid digestate for direct fertigation and recirculation. Features continuous self-cleaning action with low operating cost.
Technical Specifications
Operational metrics and parameters for standard Greliance separator systems.
| Parameter | Details |
|---|---|
| Capacity | Up to 65 m³/hr |
| Construction Material | Stainless Steel (SS304 / SS316 options) |
| Separation Type | Screw Press Compression |
| Power Range | 2.2 kW - 7.5 kW |
| Application Media | Digestate Slurry, Manure, Industrial Sludge |
| Operation Type | Continuous Automatic 24/7 |
Advantages of Greliance Solid Liquid Separator
Why dewatering slurry yields immediate operational advantages for bio-energy promoters.
| Advantage | Benefits |
|---|---|
| Efficient Dewatering | Significantly reduced moisture content in organic solid output. |
| Continuous Operation | Uninterrupted slurry feeding ensures reliable plant performance. |
| Low Maintenance | Wear-resistant screens cut down operational downtime. |
| Compact Design | Space-saving installation fits directly into pre-digester skids. |
| Odor Reduction | Minimizes foul-smelling gas escape, yielding a better working environment. |
| Easy Handling of Solids | Dry solids are easier to transport, store, bag, and sell. |
| Energy Efficient | Lower specific power consumption reduces running utility costs. |
Why Choose Greliance Separator Systems?
We deliver high-performance solutions for Bio-CNG plants, waste-to-energy projects, and industrial gas applications with a focus on efficiency, reliability, and long-term ROI.